Skip to content

Rabbit Waste Management

Reading time:  

Published: 18 June 2019
Construction and commercial waste management specialist Rabbit Waste Management Ltd has more than halved the energy required to power its shredding line, resulting in cost savings of approximately £60,000 per year.

Rabbit Waste Management is no stranger to waste shredding. The skip hire firm diverts 75,000 tonnes of locally-collected C&I, C&D and wood waste from landfill each year, in favour of manufacturing an alternative fuel used to run its own 5MW Waste to Energy Enviropower plant.

The team previously used a diesel-driven mobile shredder to process infeed materials, but when this high-speed technology failed, the hunt for a safer, more environmentally-sound and profitable replacement began.
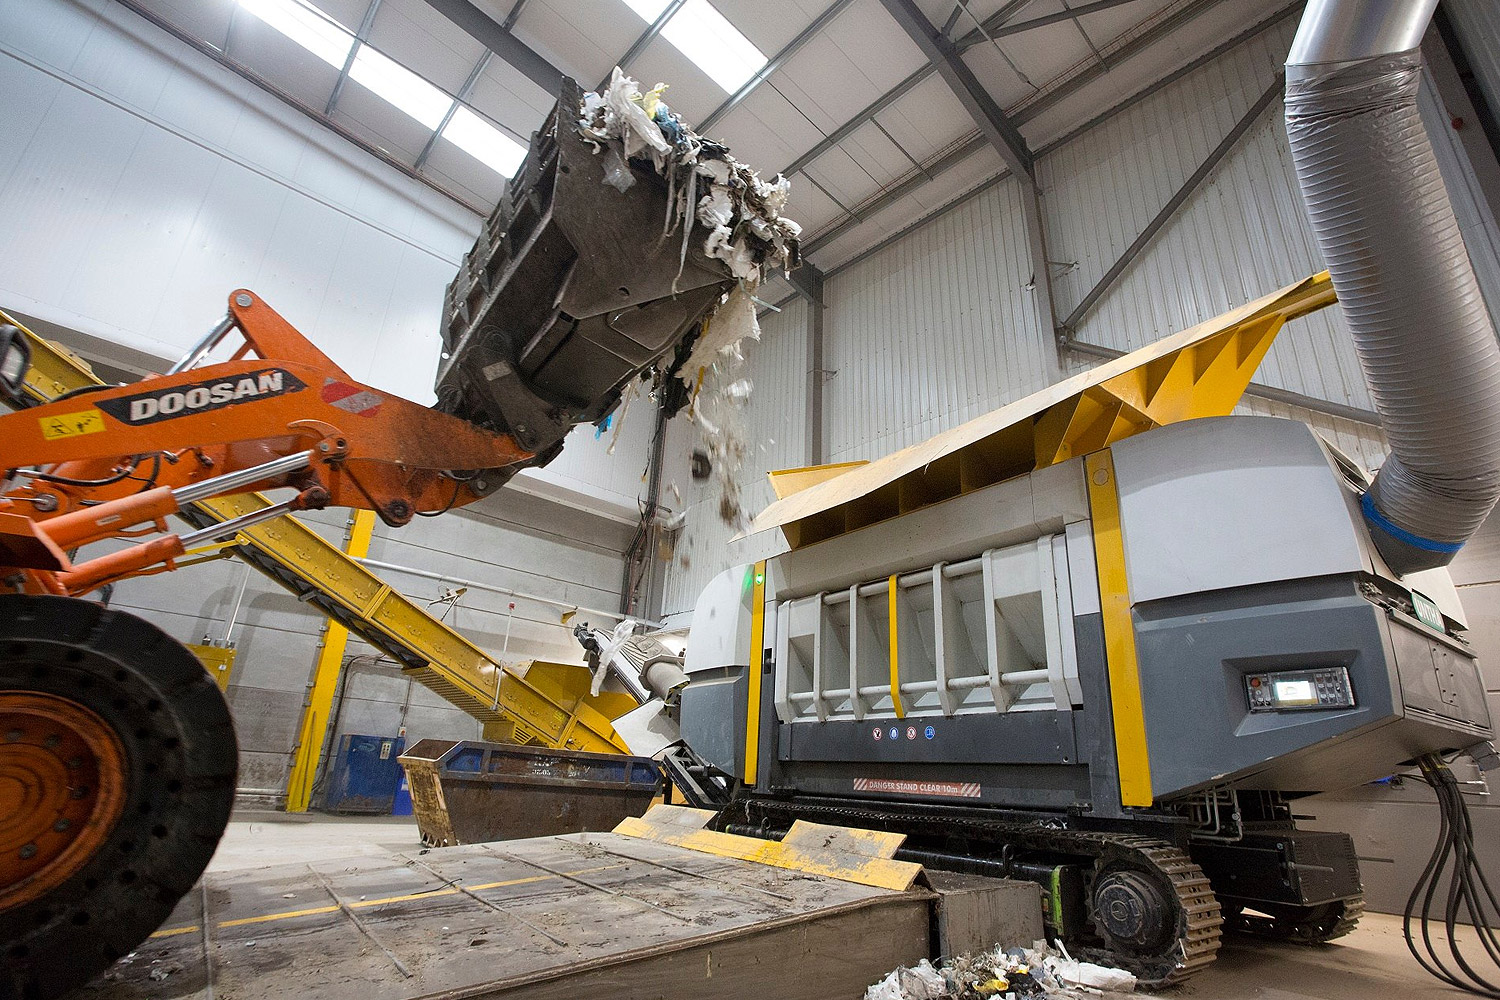
Rabbit commissioned the UNTHA XR3000C mobil-e shredder in November 2017, in a bid to lower the level of dust, fines, fire risk and noise of its waste processing operation. But the 60% reduced energy consumption has also resulted in significant financial benefits for the Sussex-based business, not to mention a much smaller net environmental impact.

The level of dust has fallen by approximately 50%, the creation of non-specification fines has dropped by 20%, and the shredder’s electric drive coupled with in-built fire protection technology, means the risk of a major incident is drastically reduced.

With 60% less energy consumption, equating to around £60,000 per year, the XR’s impact on our ‘green’ agenda – not to mention our bottom line – is vast.

Duncan Barrass, Director, Rabbit Waste Management

Download the case study

Read more about how UNTHA reinforced Rabbit Waste Management's eco-friendly values.