Skip to content

M&M Waste Solutions

Reading time:  

Published: 18 June 2019
Oxfordshire-based M&M Waste Solutions is no stranger to the resource sector. But as it started to look ahead to the next half a century, M&M sought to further boost its approach to recycling – not to mention its material recovery rate…

With a history spanning coal distribution and skip hire, M&M is a 46-year-old business that has more recently expanded into end-to-end waste collection, management and treatment, at the firm’s Materials Recycling Facility (MRF) and Waste Transfer Station in Cassington. Now handling 150,000 tonnes of materials each year, this is a significant milestone for the organisation.
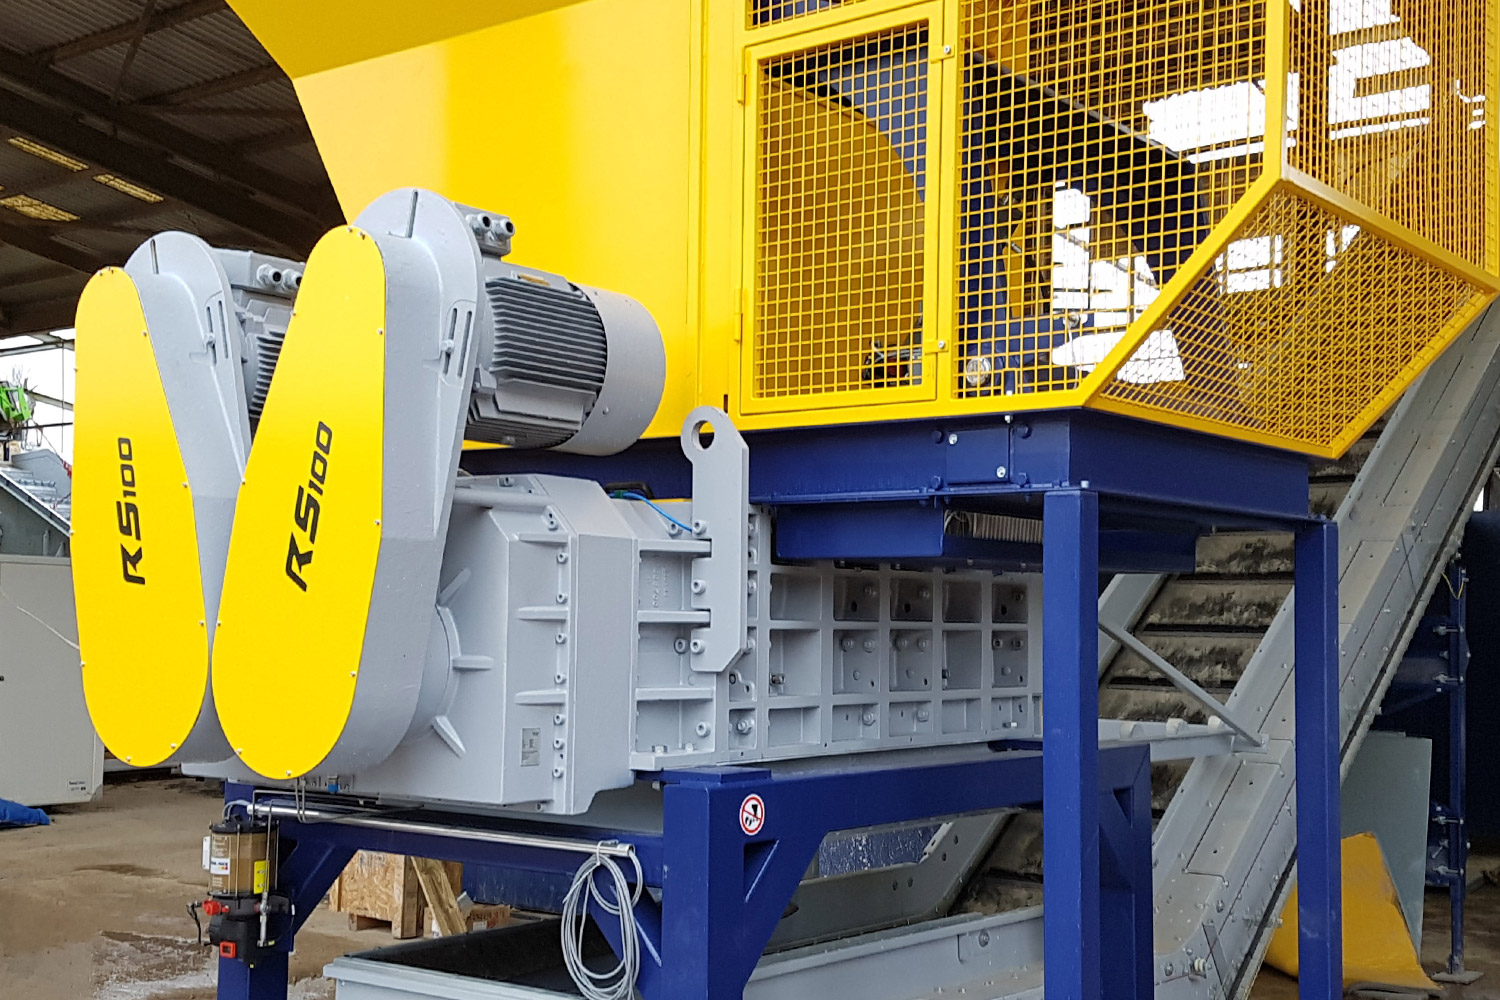
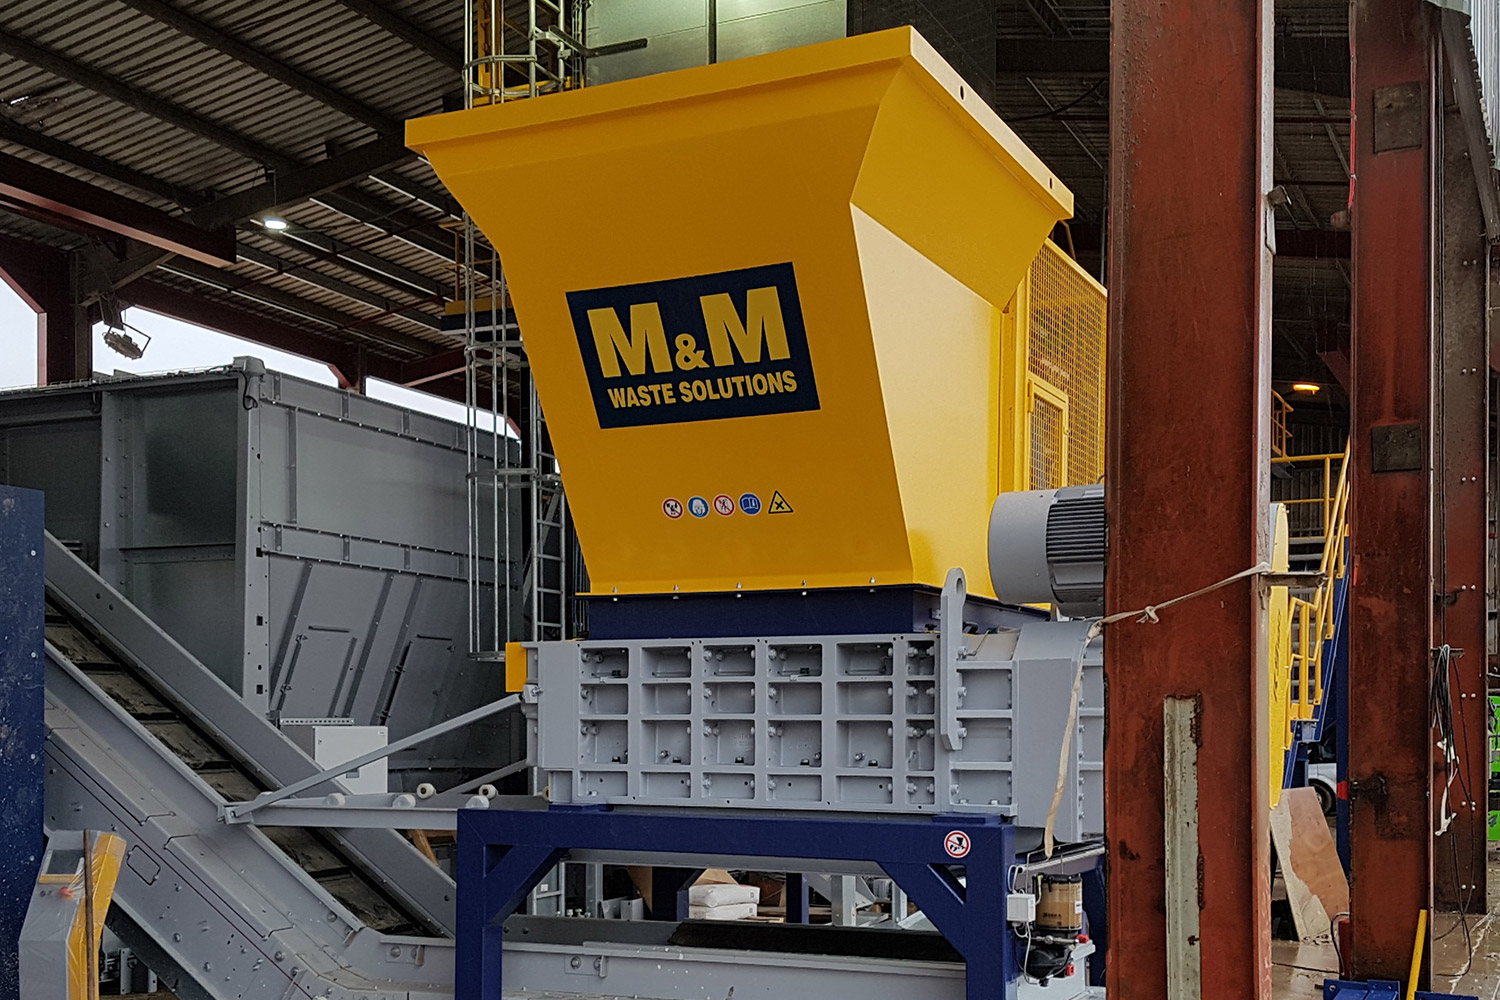
With a proven track record of boosting clients’ yield – as well as “ their recyclate quality – UNTHA led M&M through a number of shredder trials. It became clear that a four shaft RS100 shredder could comprehensively tackle the variety of materials generated at M&M’s plant.

The UNTHA shredder can produce a range of outputs depending on the material-specific liberation strategy deployed. However, M&M can now achieve a <25mm homogenous particle size, which – when handling certain materials – satisfies confidential waste shredding requirements in line with GDPR security shredding requirements.

Many of the complex materials that we’re handling – particularly from the construction and demolition industry – contain valuable composite parts that we need to ‘free’ to further boost our recycling rates. The RS100 therefore enables us to size-reduce, liberate and produce a saleable finished product for remanufacturing.

Rob Fluckiger, Managing director, M&M Waste Solutions

Download the case study

Read more about how the RS100 helped M&M Waste Solutions strive for complete resource recovery.